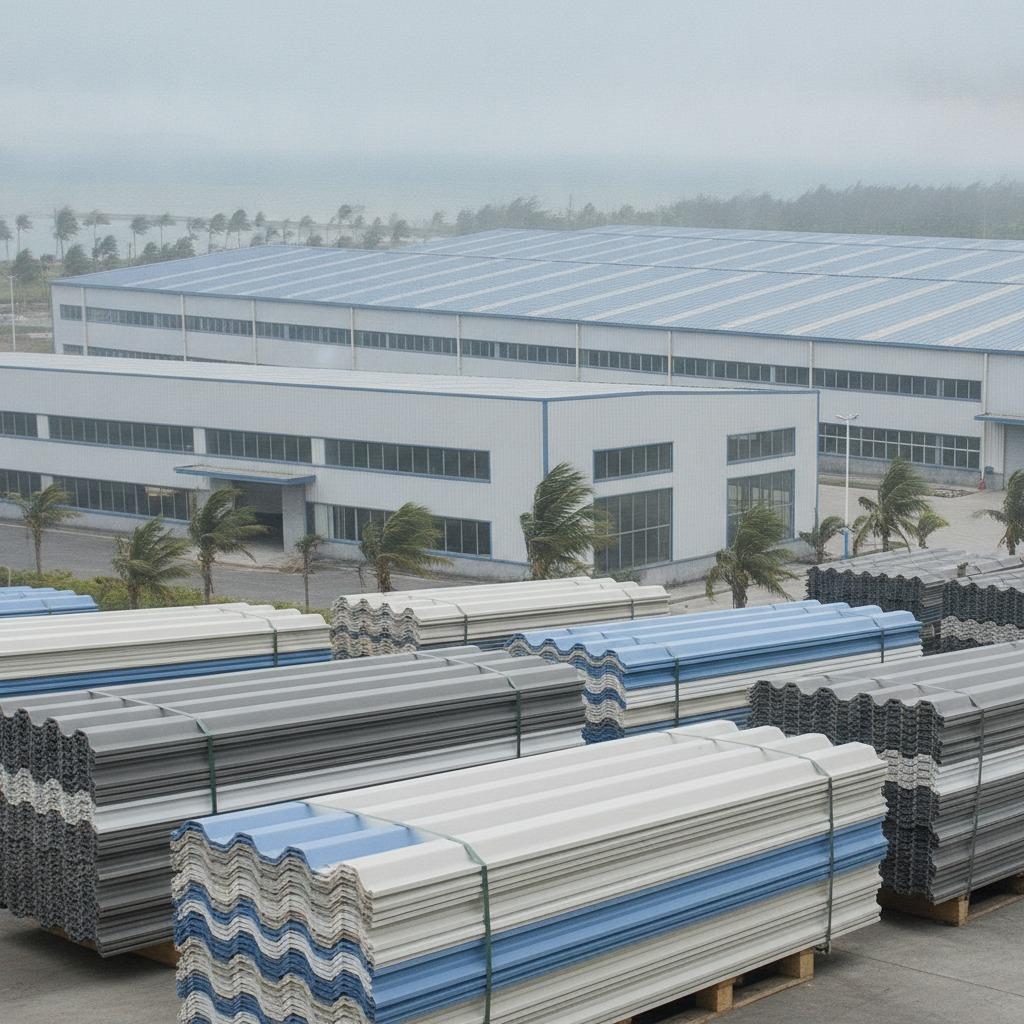
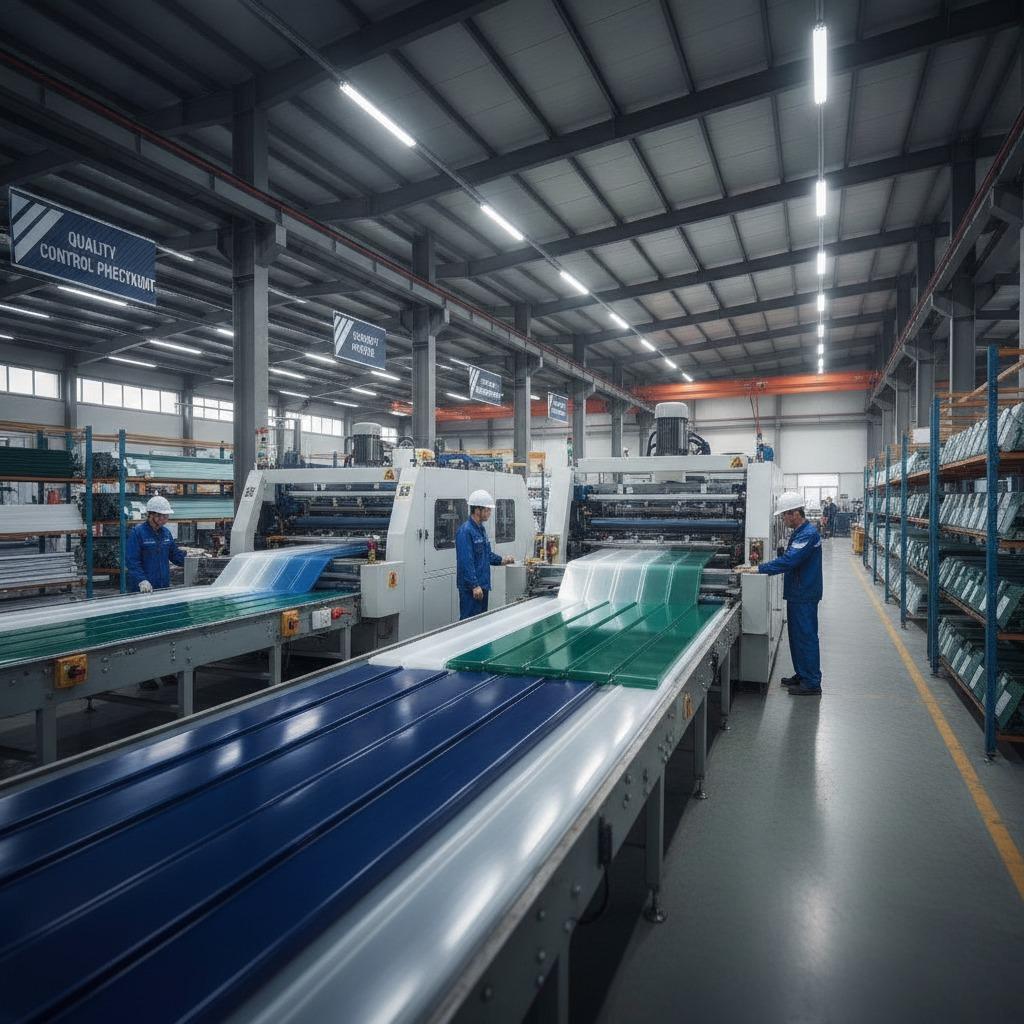
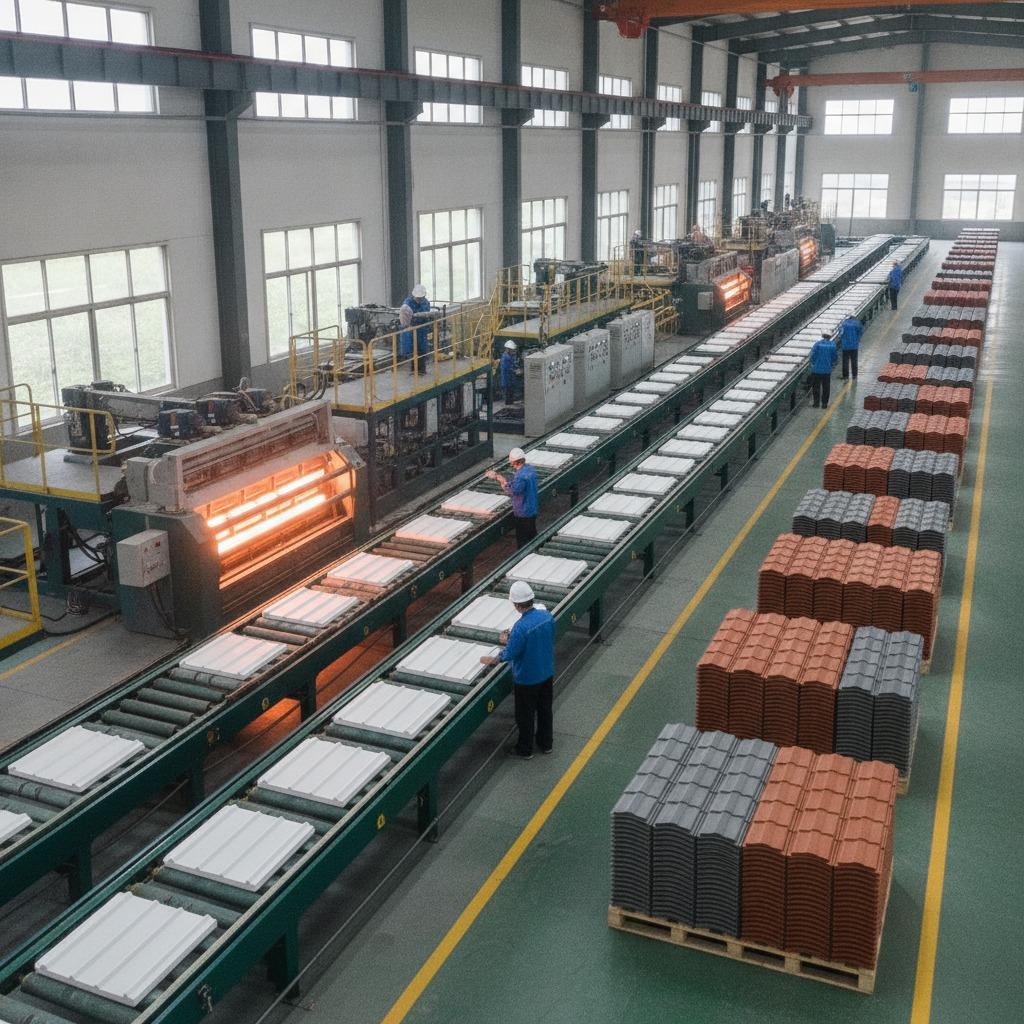
Sourcing corrugated or synthetic Spanish-style roofing profiles for coastal warehousing, fertilizer plants, or livestock facilities typically comes down to a battle against corrosion. Where galvanized sheeting rusts within five years and fiber cement cracks under thermal cycling, polymer panels offer a durable alternative. However, qualifying an ASA PVC roof tile manufacturer involves looking far beyond a glossy catalog sample. The gap between a tile that resists decades of harsh subtropical ultraviolet radiation and one that embrittles or fades within twenty-four months almost always traces back to co-extrusion discipline and resin purity.
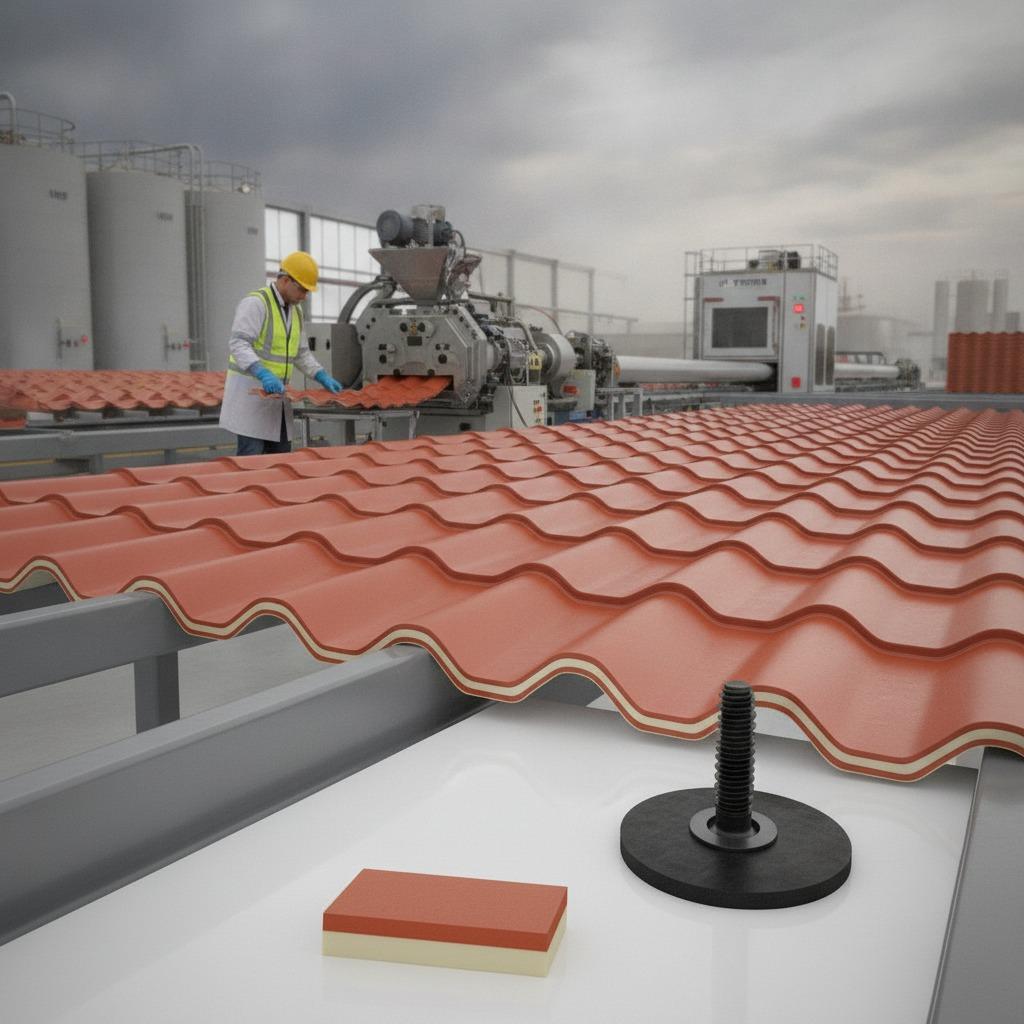
Why Co-Extruded ASA Surface Chemistry Matters
Polyvinyl chloride is inherently rigid, fire-retardant, and structurally sound when formulated with the right impact modifiers. Its fatal flaw is actinic degradation: bare PVC exposed to intense UV wavelengths gradually undergoes dehydrochlorination, turning brittle, discolored, and prone to micro-cracking. To solve this, the industry relies on Acrylonitrile Styrene Acrylate (ASA) caps.
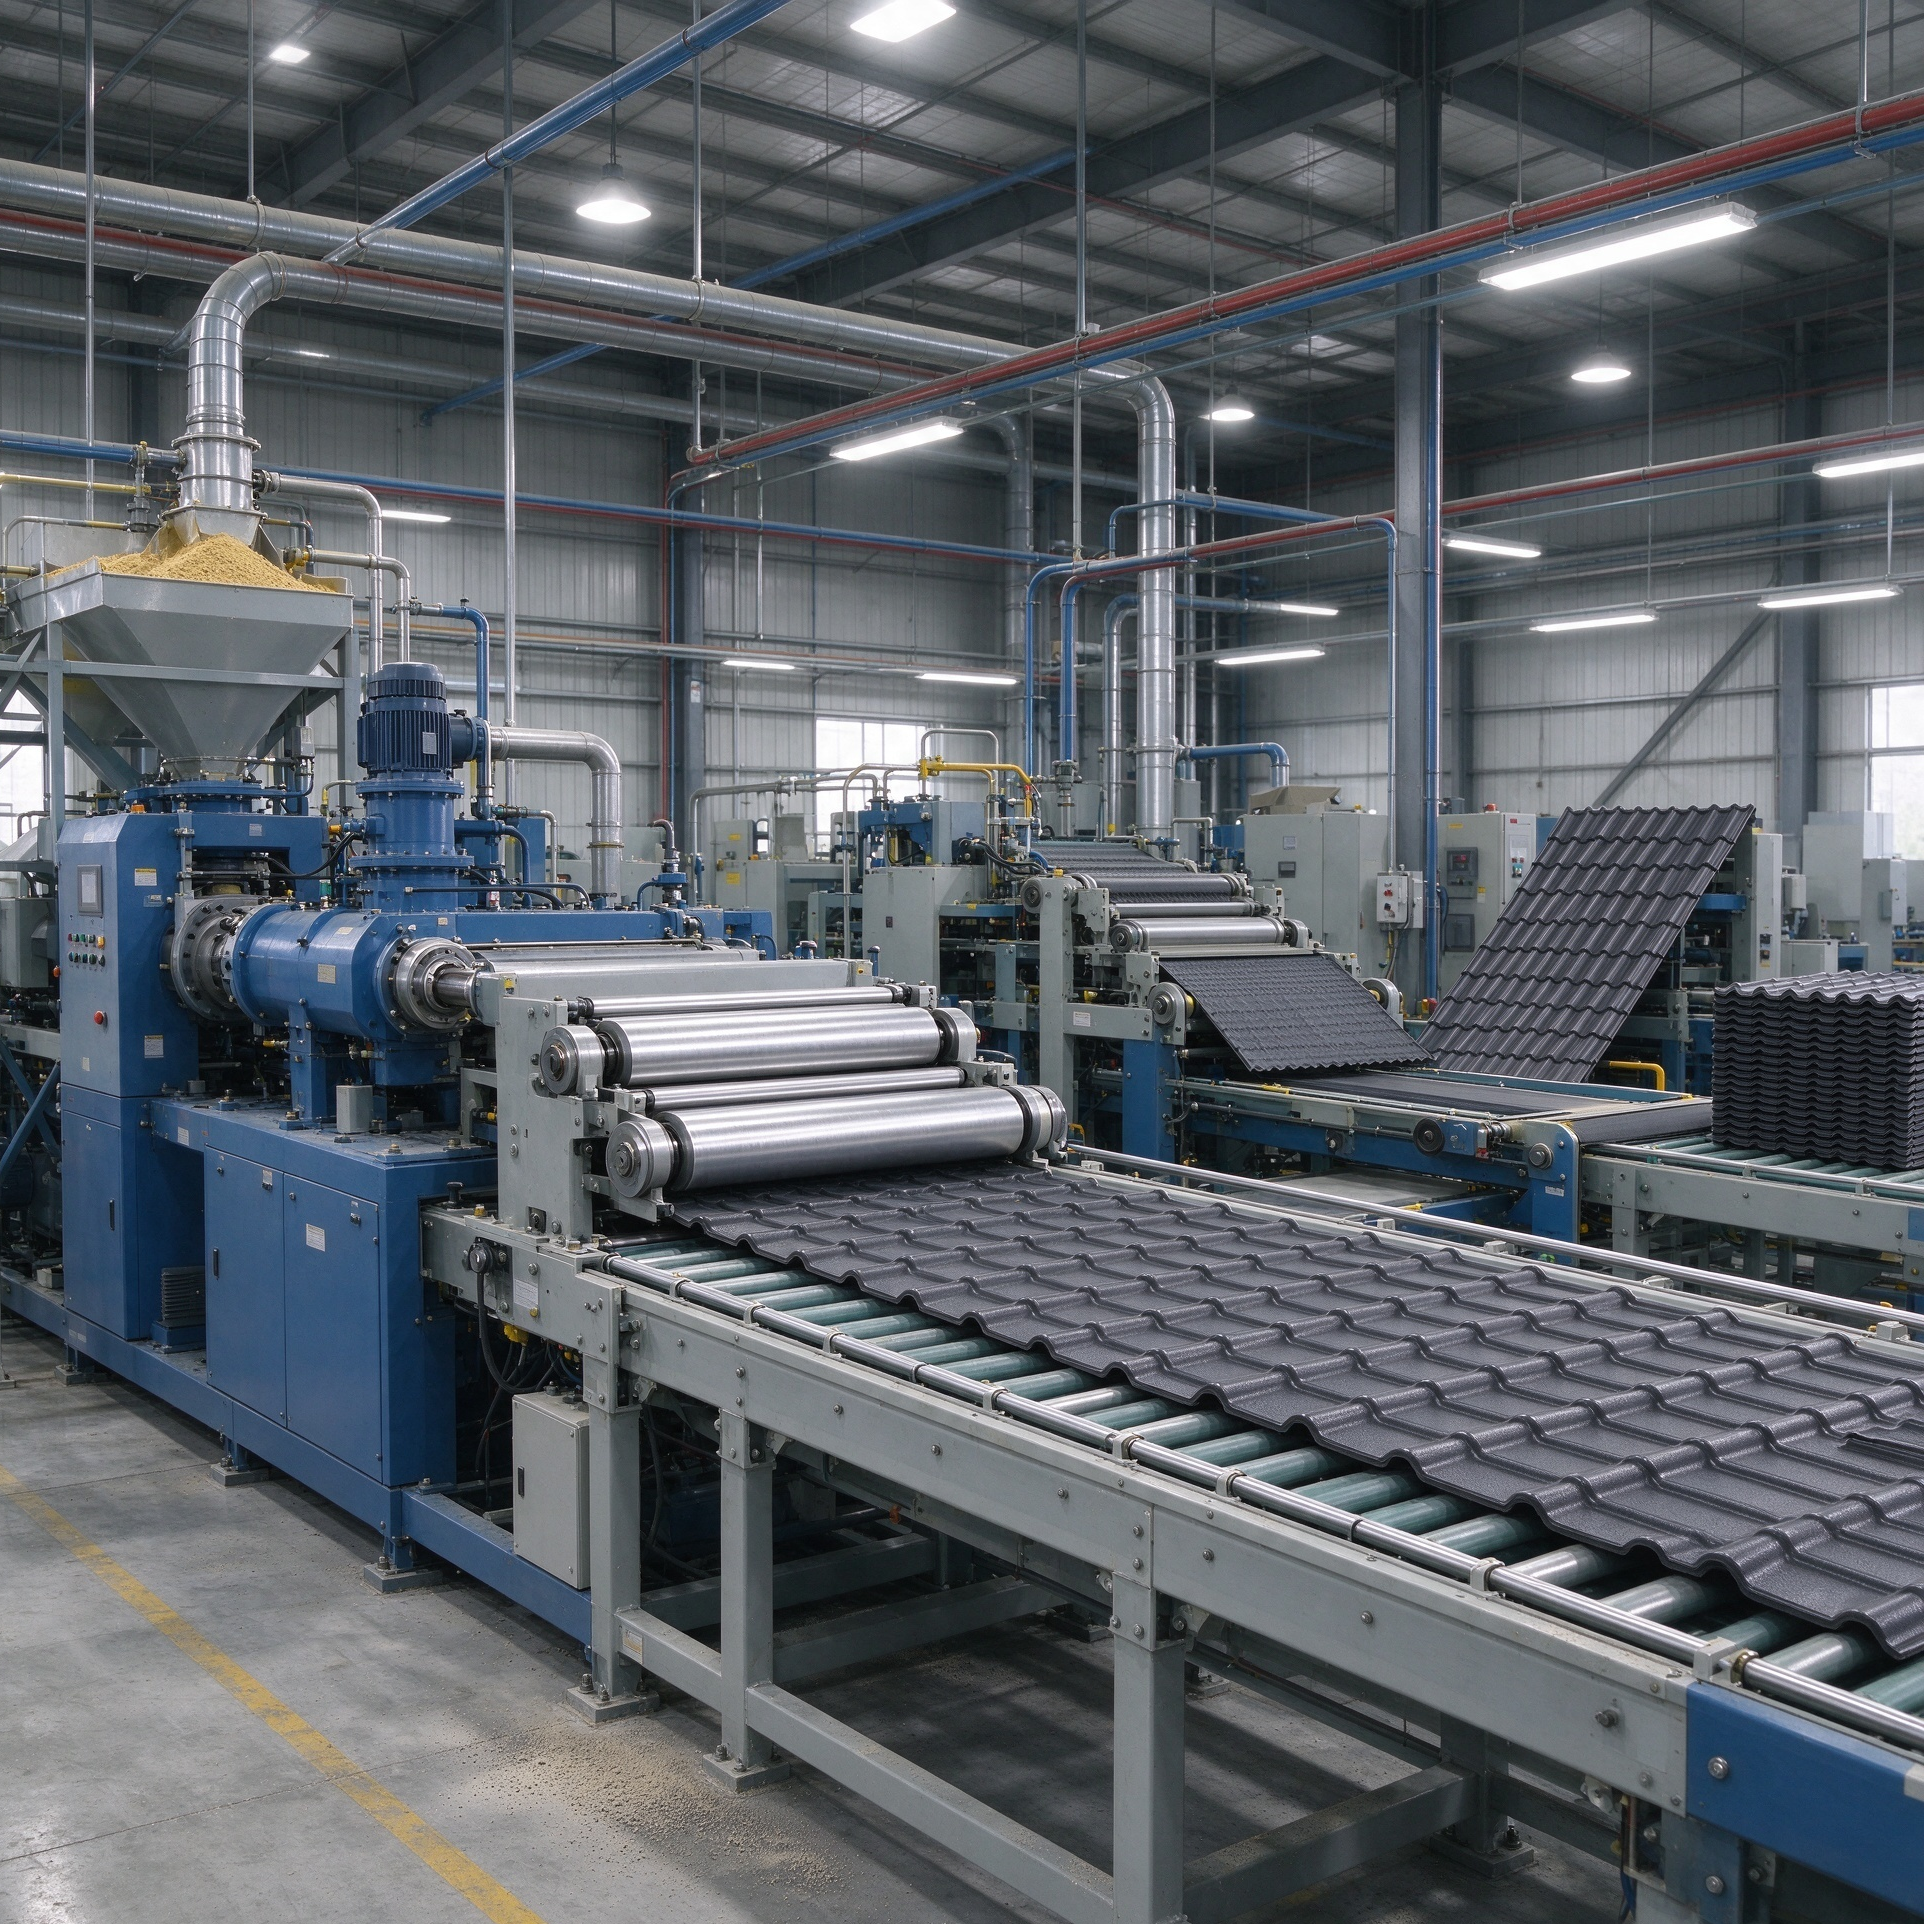
ASA is an engineering terpolymer where acrylic ester elastomer replaces the butadiene rubber found in ABS. This gives it ten times the atmospheric aging resistance of standard styrene polymers. When choosing a PVC roof tile manufacturer, the primary engineering question is how those two layers bond. A properly tuned multi-layer co-extrusion line fuses the molten ASA top skin directly to the modified PVC core without adhesives. If the manufacturer runs an unstable die temperature or skimps on the co-extruder feed block, that top layer might vary from 0.05 mm on the edges to 0.2 mm at the peak of the corrugation. Anything under 0.15 mm generally fails to deliver the promised 15-to-30-year design life in high-UV regions.
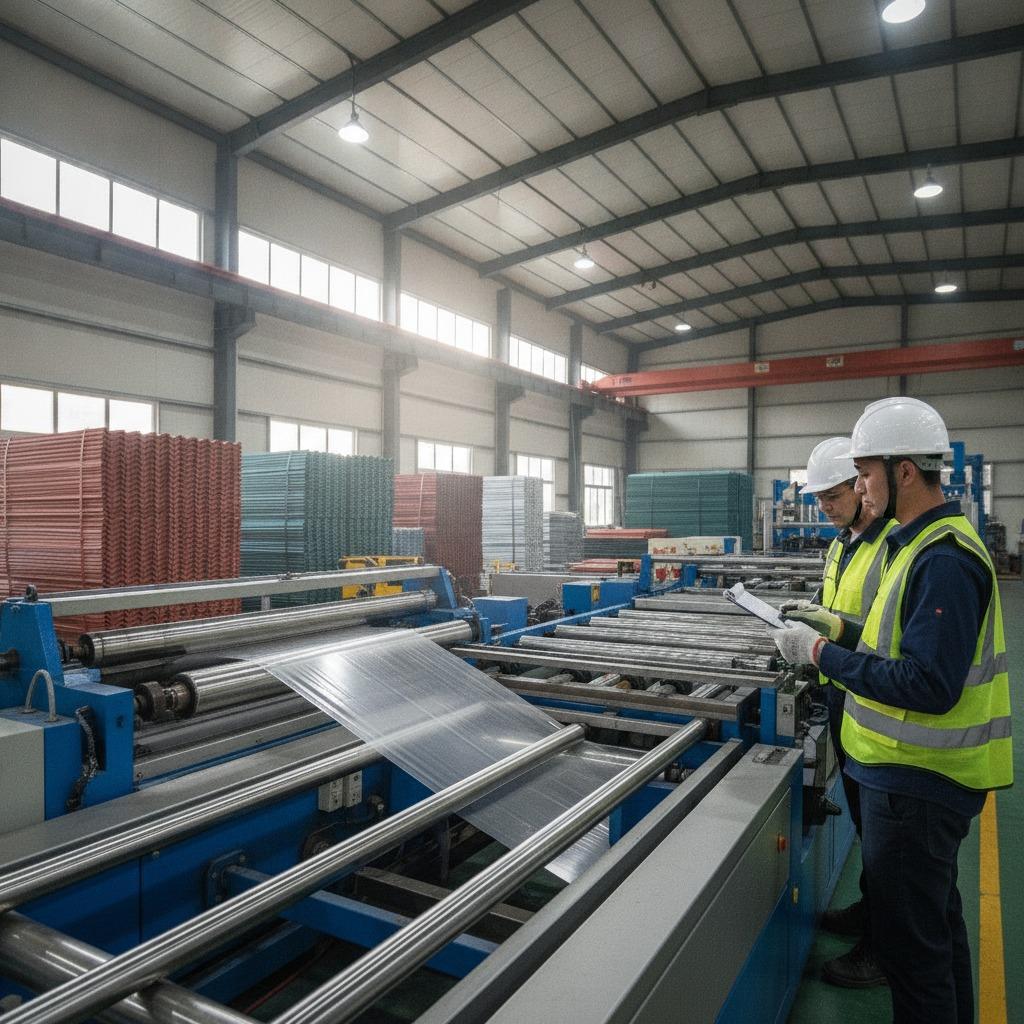
Evaluating Production Standards on the Factory Floor
Industrial buyers touring an extrusion plant should look past the neat stacking lines and head directly to the material silos and compounding room. Formulations dictate real-world structural performance far more than the profile shape.
- Virgin Resin vs. Regrind Ratios: While internal recycling of edge trim is standard practice, unscrupulous suppliers bulk out core formulations with heavy post-consumer scrap. Excess regrind degrades impact strength, making panels shatter under high winds or hail.
- Calcium Carbonate (CaCO3) Loading: Calcium carbonate is a necessary processing aid and functional filler, but it is also cheap. A reliable PVC roof manufacturer keeps ash/filler content within 15% to 25% by weight. When a compounder pushes filler above 35% to undercut pricing, the tile loses tensile elasticity and becomes fragile during winter installations.
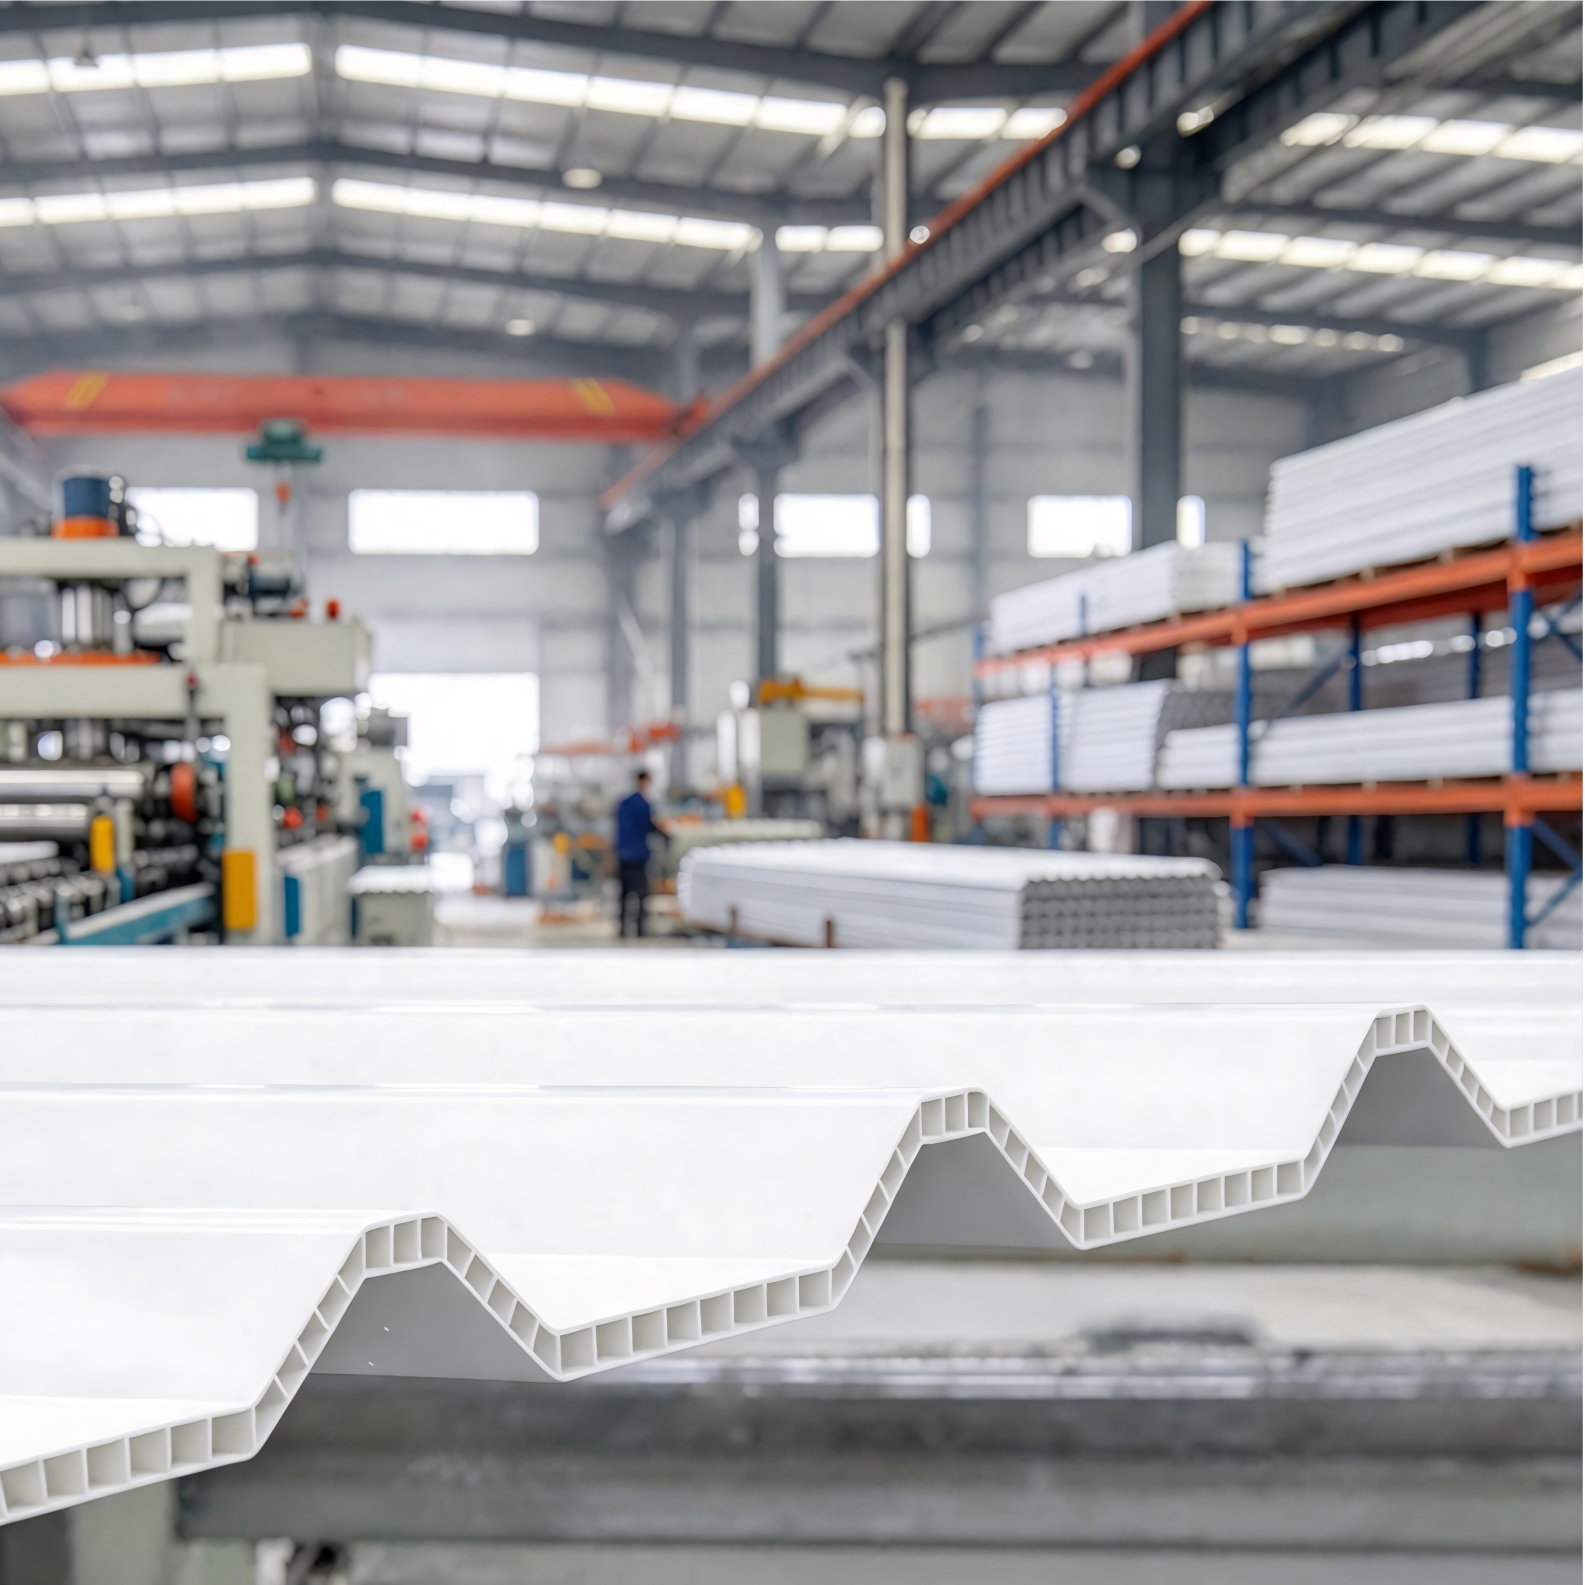
- Die Head and Tooling Maintenance: Uniform wall thickness across wide-format profiles (typically 880 mm to 1050 mm effective widths) requires precision tooling. Watch for longitudinal wall variations or telltale stress marks along profile ribs.
Common Sourcing Traps in Polymer Roofing Procurement
One frequent mistake sourcing teams make is accepting generic lab reports from an unaccredited domestic testing agency. Accelerated QUV weathering data means nothing if the tested sample had a 0.25 mm virgin ASA skin while the shipped shipping containers carry 0.08 mm skins colored with unbranded pigments.
Another blind spot is thermal expansion management. PVC has a thermal expansion coefficient around 6–8 × 10⁻⁵ /°C—substantially higher than steel. An experienced PVC roofing manufacturer will not merely sell you sheets; they will supply engineered accessories designed for movement. Fasteners must feature oversized pre-drilling specs, self-centering washers, and UV-stabilized EPDM gaskets that do not vulcanize onto the tile face. If a factory claims their panels can be rigidly screwed into purlins without thermal allowance, find another supplier immediately.
Key Technical Parameters to Specify Before Issuing a PO
To keep competing suppliers on an equal baseline, lock down your request for quotation (RFQ) with tight technical constraints rather than broad commercial claims:
- ASA Surface Layer Thickness: Specify a continuous minimum thickness (e.g., ≥ 0.15 mm or 0.20 mm measured via optical microscopy).
- Pigment Grades: Demand high-grade inorganic pigments (such as rutile titanium dioxide for light hues or ceramic mixed-metal oxides for deep terracotta and charcoal) to prevent premature chalking and shade shifting.
- Flexural and Impact Retention: Require minimum impact resistance metrics (e.g., falling dart impact testing at 0°C without crack propagation).
- Purlin Spacing Specifications: Verify load ratings across specified spans (typically 660 mm to 800 mm centers depending on sheet profile and anticipated snow or wind uplift).
Frequently Asked Questions
Can ASA PVC tiles replace corrugated metal on chemical storage warehouses?
Yes, and they are frequently preferred in those environments. Highly acidic or alkaline emissions that strip zinc galvanization or corrode prepainted steel sheets leave rigid PVC unaffected. The main limitation is operating temperature: standard formulations soften near 70°C, so facilities with intense ambient heat or uninsulated kiln exhausts require deliberate ventilation design.
How can I verify the ASA layer thickness without destructive lab gear?
A fast field check involves viewing cross-cut edges under a portable 100x digital microscope with an integrated scale. Because pure ASA differs slightly in translucence and grain from the heavily filled PVC core below it, the demarcation line is usually visible under calibrated side lighting.
What is the typical warranty standard for an industrial ASA PVC roof?
Most tier-one suppliers offer tiered warranties: typically 20 to 30 years against perforation and water ingress, combined with a separate 10-year limit on excessive color delta (usually ΔE ≤ 5 under standard outdoor exposure). Be sure the warranty explicitly names the polymer supplier for both the ASA resin and color masterbatch.
Taking the Next Step
Before issuing your next bulk purchase order, request production-run retaining samples cut directly from dynamic extrusion rather than hand-cast prototypes. Have the supplier confirm their polymer melt flow index, filler ash content, and ASA gauge control tolerance in writing within the sales contract.